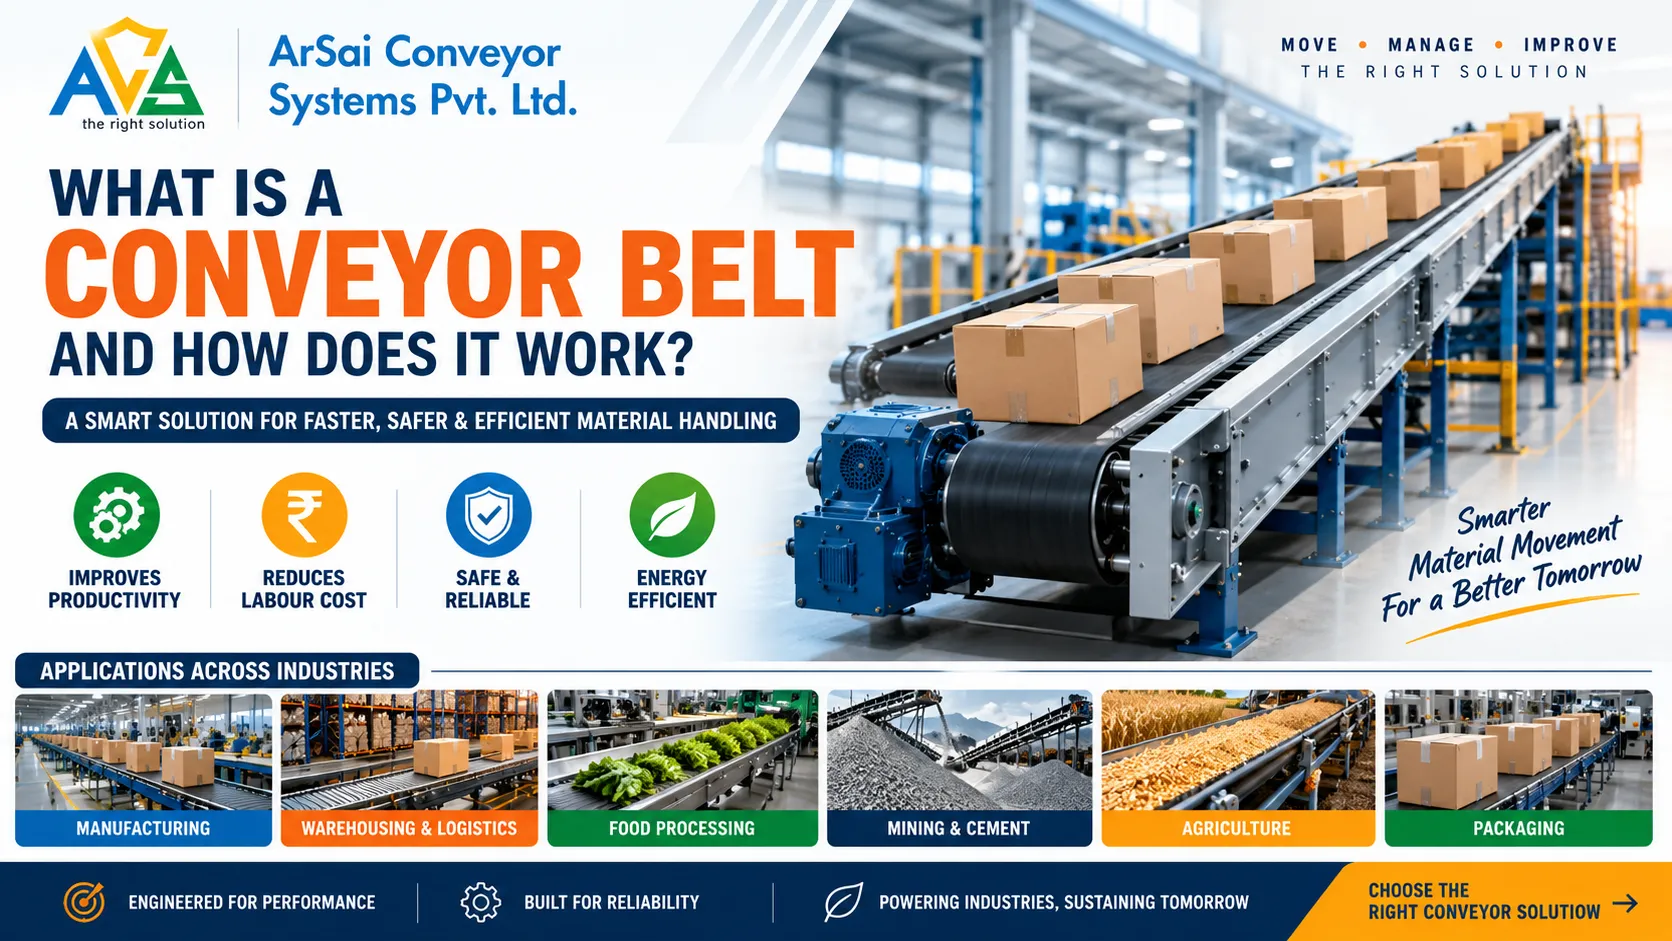
In modern manufacturing and material-handling industries, moving products and raw materials from one point to another is a routine but important task. Doing this manually can require considerable time, labour, and effort, especially when materials need to be transported continuously over long distances. This is where a conveyor belt becomes an essential part of industrial automation.
A conveyor belt is a continuous moving belt used to transport products, components, packages, and bulk materials from one location to another. Depending on the design, it can be used for horizontal transportation, inclined movement, feeding, sorting, loading, unloading, and production-line applications. Belt conveyor systems are widely used in manufacturing, warehouses, logistics, mining, food processing, packaging, agriculture, and many other industries.
For businesses planning to install a material-handling system, understanding what is conveyor belt, how it works, its components, types, and applications can help in selecting the right solution.
A Brief History of the Conveyor Belt
Conveyor belts have been part of industrial material handling for well over a century, with early leather and canvas belt systems used in mining and agriculture in the late 1800s. The introduction of rubber and fabric-reinforced belting in the early 20th century, followed by the rise of powered assembly lines, turned conveyors into a core part of modern manufacturing. Today’s belts — built from rubber, PVC, modular plastic, and specialised materials — are a direct evolution of that original concept: a continuous moving surface that removes the need to carry material by hand.
What Is a Conveyor Belt?
A conveyor belt is the continuous carrying surface of a belt conveyor system. It normally runs in an endless loop around two or more pulleys. One pulley is powered by a motor and transfers movement to the belt, while other pulleys support, guide, or tension the belt. Rollers or idlers are generally used underneath the carrying side to support the load.
The belt itself can be manufactured from different materials depending on the application. Rubber, PVC, fabric-reinforced materials, metal, and other specialized materials can be used for different operating conditions. The selection depends on factors such as load, product type, temperature, speed, moisture, abrasion, and working environment.
You may also come across searches such as conver belt, convery belt, or conveyer belt. These are commonly used spelling variations of the term “conveyor belt,” but the correct industry term is conveyor belt.
Also Read: How to Increase the Lifespan of an Industrial Conveyor Belt
How Does a Conveyor Belt Work?
The working principle of a conveyor belt is relatively simple. The belt forms a continuous loop around the conveyor pulleys. A motor provides power to the drive pulley, which causes the belt to move. Products or materials placed on the moving surface are carried along the conveyor toward the discharge point.
The basic operating process can be understood in a few stages.
First, an electric motor supplies rotational power to the drive mechanism. A gearbox may be used to obtain the required speed and torque.
Next, the drive pulley rotates and pulls the continuous belt around the conveyor frame. The belt moves over supporting idlers or rollers.
Material is then loaded onto the carrying side of the belt. As the belt moves, the material travels with it until it reaches the required discharge location.
After unloading, the belt returns along the return side of the conveyor and continues the cycle.
This continuous movement allows industries to transport materials at a controlled and consistent rate.
What Speed Do Conveyor Belts Run At?
Conveyor belt speed depends heavily on the application, the material being handled, and the type of conveyor. Light-duty conveyors used for packaging or assembly-line work typically run in the range of 20 to 100 feet per minute (FPM), which is roughly 0.1 to 0.5 metres per second — slow enough for manual inspection or hand assembly alongside the belt. Standard industrial and material-handling conveyors commonly operate between 100 and 400 FPM (0.5 to 2 m/s). Heavy-duty bulk material conveyors, such as those used in mining, cement, or aggregate handling, can run considerably faster, depending on load capacity and incline.
The right speed is selected based on required throughput, product fragility, belt width, and the load the conveyor needs to carry — a speed that works well for cartons on a packaging line would be unsuitable for delicate components on an assembly conveyor.
Control Systems and Automation in Conveyor Belts
A modern conveyor belt rarely runs as a standalone mechanical system. In most industrial setups, the conveyor is connected to a control panel, a Programmable Logic Controller (PLC), or a computer-based system that manages its start, stop, speed, and direction. This level of automation allows a conveyor to work in sync with other machines on the production line rather than operating in isolation.
Speed Control
Conveyor speed is usually regulated using a Variable Frequency Drive (VFD) or a Variable Speed Drive (VSD). These devices adjust the motor’s power supply to speed the belt up or slow it down, which is useful for handling fragile products carefully, matching the pace of upstream and downstream machines, or fine-tuning output during high-volume production.
Direction Control
Certain conveyor systems are built to run in both directions. Reversing the motor’s rotation allows the belt to move material back and forth between two points, which is helpful in sorting operations, buffer storage, or facilities where the same conveyor line serves more than one process.
Sensors and Feedback Loops
Photoelectric sensors, proximity sensors, load cells, and encoders are commonly fitted along a conveyor to track the presence of material, detect belt misalignment, and monitor load weight. This real-time feedback lets the control system make automatic adjustments — slowing the belt, triggering an alarm, or stopping the line — before a small issue like a jam or a tracking fault turns into downtime.
Safety Controls
Emergency stop buttons, pull-cord switches, guarding, and interlocks are standard on industrial conveyor systems. These allow the conveyor to be stopped immediately in the event of an emergency, protecting both operators and the material being handled.
Main Components of a Conveyor Belt System
Although a conveyor may appear simple from the outside, several components work together to provide smooth material movement.
Conveyor Belt
The belt is the primary carrying component. Its construction is selected according to the weight and characteristics of the material being transported.
Drive Pulley
The drive pulley is connected to the motor and transfers the required movement to the belt. Its size and surface design can influence belt performance.
Tail Pulley
The tail pulley is generally positioned at the opposite end of the conveyor and helps guide the belt around the system.
Idlers and Rollers
Idlers support the belt and the material placed on it. Different arrangements can be used depending on whether the conveyor is transporting unit loads or bulk materials.
Motor and Gearbox
The motor provides power, while the gearbox can reduce speed and increase torque according to the conveyor’s operating requirements.
Conveyor Frame
The frame supports the belt, pulleys, rollers, drive system, and other components. It can be designed according to the conveyor length, load, and installation environment.
Take-Up Arrangement
A take-up system maintains suitable belt tension. Proper tension is important for stable operation and effective power transmission.
Different Types of Conveyor Belts
There is no single conveyor belt design suitable for every industry. Different belt configurations are developed for specific materials and operating requirements.
Flat Belt Conveyor
Flat belt conveyors are commonly used for transporting boxes, packages, components, and other unit loads. They are particularly useful in manufacturing, assembly, packaging, and warehouse applications.
Cleated Belt Conveyor
Cleated belts include raised sections or cleats across the belt surface. These can help prevent products or bulk materials from sliding backward when the conveyor is inclined.
Inclined Belt Conveyor
An inclined conveyor transports materials between different elevations. It can be useful for moving products from one production level to another or feeding materials into processing equipment.
Troughed Belt Conveyor
Troughed conveyors use specially arranged idlers to create a trough-like carrying surface. This design is often used for bulk materials such as minerals, aggregates, grains, coal, and other loose products.
Modular Belt Conveyor
Modular belts consist of interlocking sections and can be useful in applications requiring easy cleaning, maintenance, or belt replacement.
The appropriate conveyor design depends on the product, capacity, speed, distance, inclination, environment, and production process.
Sandwich Belt Conveyor
A sandwich belt conveyor uses two belts facing each other that move in the same direction, holding the material securely between them. This design is useful for transporting material on steep inclines or even vertically, where a single-belt conveyor would cause the load to slip or roll back.
Curve Belt Conveyor
Curve belt conveyors are built to move products around bends rather than in a straight line. They use flexible belting that can bend and twist to follow a curved path, which is useful in facilities where space constraints require the conveyor line to change direction without a separate transfer point.
Where Are Conveyor Belts Used?
One of the biggest advantages of conveyor systems is their versatility. They can be designed for lightweight packages as well as heavy industrial materials.
In manufacturing plants, conveyor belts can transfer components between different production stages. They can also connect machines and reduce manual material movement.
In warehouses and logistics centers, conveyors help move cartons, parcels, boxes, and packages between storage, sorting, packing, and dispatch areas.
In food processing, specialized conveyor belts can transport food products through processing, inspection, cooling, packaging, and other stages.
In mining and bulk-material handling, heavy-duty conveyor systems can transport materials over significant distances. Conveyor belts are also used in cement, power, steel, agriculture, and aggregate-handling applications.
Benefits of Using a Conveyor Belt
A properly designed conveyor belt system can provide several operational advantages.
Reduced manual handling: Materials can be transported automatically instead of being moved manually between workstations.
Continuous operation: Conveyor systems can provide a consistent flow of materials throughout a production or handling process.
Improved productivity: Faster and more predictable material movement can help production lines maintain a steady workflow.
Better workplace organization: A dedicated transportation route can reduce unnecessary movement of workers and materials.
Flexible design: Conveyors can be designed for different lengths, widths, speeds, elevations, and layouts.
Suitable for automation: Sensors, controls, weighing systems, diverters, and other equipment can be integrated into conveyor systems for more advanced material handling.
How to Choose the Right Conveyor Belt?
Selecting a conveyor should start with understanding the material being transported. Product weight, dimensions, surface characteristics, temperature, moisture, and abrasiveness can all influence belt selection.
The required capacity is another important consideration. A conveyor designed for a low material flow may not be suitable for a high-throughput application.
Conveyor length and inclination should also be evaluated. If the system needs to transport products upward, a suitable belt surface or cleated arrangement may be necessary.
Operating speed is equally important. A high-speed conveyor may be useful for certain automated production lines, while slower speeds may be preferable for manual inspection, assembly, or fragile products.
The operating environment should also be considered. Food-processing, chemical, outdoor, dusty, humid, and high-temperature environments may require different belt materials and construction.
Conveyor Belt Maintenance
Regular maintenance can help extend the operating life of a conveyor system. Belt alignment should be checked because tracking problems can cause uneven wear or belt damage.
Pulleys, rollers, bearings, and drive components should also be inspected periodically. Any unusual noise, vibration, slipping, or belt movement should be investigated before it develops into a larger problem.
Cleaning is especially important in food, pharmaceutical, packaging, and dusty industrial environments. The maintenance schedule should be based on operating hours, material characteristics, and the manufacturer’s recommendations.
Why Choose a Professional Conveyor Manufacturer?
A conveyor is not simply a belt mounted on rollers. Its performance depends on correct engineering of the belt, drive system, frame, pulleys, rollers, tensioning arrangement, and controls.
A professional manufacturer can evaluate the material, required capacity, conveyor dimensions, operating conditions, and production layout before developing the appropriate system.
For businesses looking for reliable material-handling solutions, Overhead Conveyor provides industrial conveyor solutions designed for different material-handling requirements.
Conclusion
A conveyor belt is one of the most practical material-handling solutions used in modern industry. It works by continuously circulating a belt around pulleys, with a powered drive mechanism moving the belt and carrying materials from one location to another.
From manufacturing and packaging to warehouses, food processing, mining, agriculture, and heavy industries, conveyor systems can reduce manual handling and create a more consistent flow of materials.
If you were wondering what is conveyor belt, the simplest answer is that it is a continuous material-carrying system designed to move products or materials efficiently. Whether you search for conver belt, convery belt, or conveyer belt, the industrial concept remains the same—the correct term is conveyor belt.
The key to getting the best performance, however, is choosing a conveyor system according to the actual application. Belt material, load capacity, speed, dimensions, inclination, operating environment, and maintenance requirements should all be considered before installation. With the right design and regular maintenance, a conveyor belt can become an important part of an efficient and dependable industrial material-handling system.