Modern manufacturing facilities handle a large number of products and components every day. Moving these materials manually between different workstations can take time, require more labor, and increase the chances of product damage. Overhead conveyors provide a practical solution by transporting materials above the production floor while keeping valuable floor space available for other activities.
These conveyor systems are commonly used in automotive plants, paint shops, fabrication units, warehouses, food-processing facilities, and general manufacturing industries. Depending on the application, businesses can choose from different conveyor configurations, including trolley conveyors, continuous systems, and power and free conveyors.
In this guide, we will understand how overhead conveyor systems work, their major types, components, applications, design considerations, and key benefits.
What Is an Overhead Conveyor?
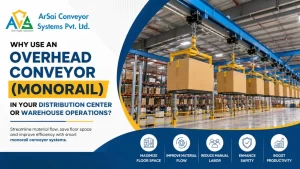
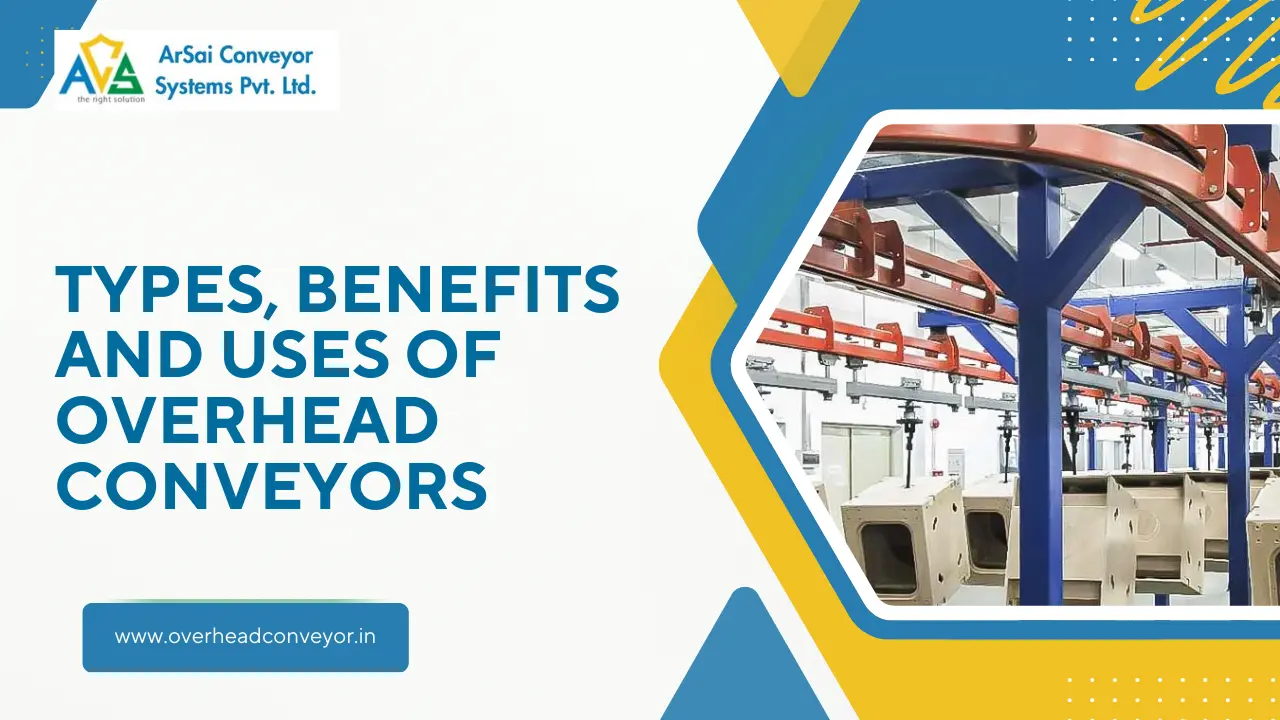
An overhead conveyor is a material-handling system designed to transport products, parts, or loads along an elevated path. Instead of occupying floor space like a conventional belt or roller conveyor, the conveying mechanism is installed above the working area.
An overhead conveyor track provides the route along which carriers, trolleys, or other load-supporting devices move. The load is suspended from the conveyor and transported from one location to another.
This arrangement is particularly useful when floor space is limited or when products need to pass through several processing stages.
An overhead conveyor can also be integrated with production lines, storage areas, washing systems, painting booths, drying ovens, assembly stations, and inspection areas.
How Do Overhead Conveyor Systems Work?
The basic working principle is straightforward. A motorized drive arrangement moves a chain, trolley, or carrier along a fixed overhead track. Products are attached to or placed on carriers that travel with the conveyor.
The conveyor may operate continuously or allow individual carriers to stop at selected locations, depending on the system design.
A typical material movement process looks like:
Loading → Overhead Transportation → Processing/Workstation → Unloading
The exact movement pattern depends on the type of conveyor, product weight, required speed, production layout, and automation level.
Types of Overhead Conveyor Systems
There are several types of overhead conveyor systems, and each is designed for different production and material-handling requirements.
1. Overhead Trolley Conveyor
An overhead trolley conveyor uses trolleys or carriers that move along an elevated track. Products are suspended from these trolleys and transported through the facility.
These systems are suitable for applications where products need to remain suspended during transportation. They are often used for automotive components, fabricated parts, garments, and other products that can be easily hung from carriers.
2. Continuous Overhead Conveyor
A continuous overhead conveyor moves carriers along a predetermined route at a relatively consistent pace. It is useful for production environments where products need to move continuously between different operations.
This type of system can help maintain a steady material flow and reduce unnecessary manual handling.
3. Power and Free Conveyor
A power and free conveyor provides greater flexibility than a conventional continuous conveyor. Its carriers can be powered along the track while also being stopped, accumulated, or redirected when required.
This makes power and free systems useful for complex production lines where different products may require different processing times.
For example, a carrier can stop at a workstation while other carriers continue moving along the production route. This flexibility makes power and free conveyors popular in automotive and industrial manufacturing.
4. Monorail Overhead Conveyor
A monorail system uses a single continuous track through which carriers or trolleys travel. Its relatively simple route makes it suitable for applications involving repetitive transportation between defined points.
Monorail systems can also be designed with curves, inclines, and declines where required by the facility layout.
Major Overhead Conveyor Parts
Understanding the main overhead conveyor parts is important when selecting or maintaining a system. Although the exact configuration varies, common components include:
- Conveyor track
- Chain or traction mechanism
- Trolleys
- Load carriers
- Drive unit
- Motor and gearbox
- Sprockets
- Take-up arrangement
- Track supports
- Switches and transfer sections
- Loading and unloading stations
- Safety guards and protective devices
The quality and compatibility of these components can directly affect conveyor performance, reliability, and maintenance requirements.
What Is an Overhead Conveyor Track?
The overhead conveyor track is the structural pathway that guides the trolleys or carriers throughout the conveying route. It can be arranged in straight sections, curves, inclines, declines, and other configurations according to the plant layout.
The track must be appropriately designed to handle the expected load, operating speed, environmental conditions, and movement pattern.
For demanding applications, factors such as temperature, dust, chemicals, humidity, and continuous operation should also be considered when selecting the track and other components.
Overhead Conveyor Design Considerations
Effective overhead conveyor design starts with understanding the actual material-handling requirement. Installing a conveyor without properly analyzing the production process can lead to inefficient movement and unnecessary operating costs.
Some important design factors include:
Load Capacity
The conveyor should be capable of safely carrying the maximum expected load. Both individual load weight and the number of carriers operating simultaneously should be considered.
Conveyor Speed
The required speed depends on production volume and processing time. Some applications require slow movement for painting or washing, while others may require faster transportation.
Track Layout
The track should follow the most efficient route through the facility. Curves, elevation changes, switches, and transfer points need to be planned carefully.
Product Characteristics
Product dimensions, shape, weight, surface condition, and method of hanging or attachment all influence the carrier design.
Operating Environment
Paint shops, foundries, food-processing facilities, and chemical plants may have very different environmental conditions. Conveyor materials and components should be selected accordingly.
Applications of Overhead Conveyors
Overhead conveyors are used in many industries because they can transport products while keeping the floor relatively clear.
Common applications include:
- Automotive manufacturing
- Auto component handling
- Paint and powder coating plants
- Surface treatment facilities
- Fabrication industries
- Welding and assembly lines
- Food-processing facilities
- Warehouses and distribution centers
- Garment manufacturing
- Industrial washing systems
- Drying and curing lines
- Material transfer between production stations
In paint shops, for example, an overhead conveyor can transport components through cleaning, pretreatment, painting, drying, and inspection stages without requiring workers to move the parts manually between each station.
Benefits of Overhead Conveyors
1. Better Use of Floor Space
Since the conveyor operates above the floor, valuable production space can remain available for machines, workers, storage, and other operations.
2. Reduced Manual Handling
Products can move automatically between workstations, reducing the need for workers to repeatedly carry heavy or awkward components.
3. Improved Production Flow
A properly planned conveyor creates a predictable movement path, helping maintain a more organized production process.
4. Suitable for Continuous Operations
Overhead systems can operate for extended periods and can be integrated with automated production processes.
5. Flexible Layout
Depending on the configuration, the conveyor can travel through straight sections, curves, inclines, and declines.
6. Better Product Movement
Suspending products can reduce contact with the floor and minimize certain types of handling-related damage or contamination.
7. Easy Integration
Overhead conveyor systems can be integrated with painting, washing, drying, assembly, inspection, and other industrial processes.
How to Select the Right Overhead Conveyor?
Choosing the right system requires more than comparing prices. Consider the product weight, dimensions, required capacity, conveyor speed, route length, operating environment, and required automation level.
For simple repetitive transportation, a trolley or monorail arrangement may be sufficient. For production lines where carriers need to stop, accumulate, or move at different stages, a power and free conveyor can provide greater flexibility.
It is also important to work with an experienced conveyor manufacturer that can evaluate the plant layout and develop a system around the actual application.
Why Choose Overhead Conveyor Systems?
We provides industrial conveyor solutions designed around specific material-handling requirements. Every production facility has different space limitations, product characteristics, and workflow requirements, so conveyor design needs to be approached accordingly.
A properly engineered overhead conveyor can help improve material movement, reduce manual handling, and create a more organized production environment. From track layout and carrier selection to drive arrangements and integration with other equipment, each element contributes to the overall performance of the system.
Conclusion
Overhead conveyors are an efficient material-handling solution for industries that need to move products through a defined production or processing route while preserving valuable floor space. From basic trolley conveyors to flexible power and free systems, different configurations are available for different applications.
Understanding the overhead conveyor parts, track arrangement, load requirements, operating conditions, and production workflow is essential for selecting the right system. With proper overhead conveyor design, these systems can provide reliable material movement and integrate smoothly with modern industrial processes.
For businesses looking to improve production flow and reduce manual transportation, an appropriately designed overhead conveyor system can be a valuable long-term investment.