Roller Conveyor Manufacturer in Panipat
A Roller Conveyor Manufacturer in Panipat provides efficient material movement solutions for factories, warehouses, packaging units, and logistics facilities. Roller conveyors are designed to move cartons, boxes, pallets, trays, containers, and other suitable loads through a defined path, making them useful wherever frequent manual transportation is involved.
In an industrial setup, smooth material flow can save handling time and keep different work areas better connected. Roller conveyor systems can be configured according to the size and weight of the product, available floor space, conveying distance, and required movement speed. The choice of roller diameter, spacing, frame construction, and conveyor width can be adjusted to suit the application.
From production and assembly areas to packing and dispatch sections, roller conveyors can support different stages of internal material handling. Depending on the workflow, businesses can choose a gravity-based system for simple movement or a powered arrangement when controlled transportation is required.
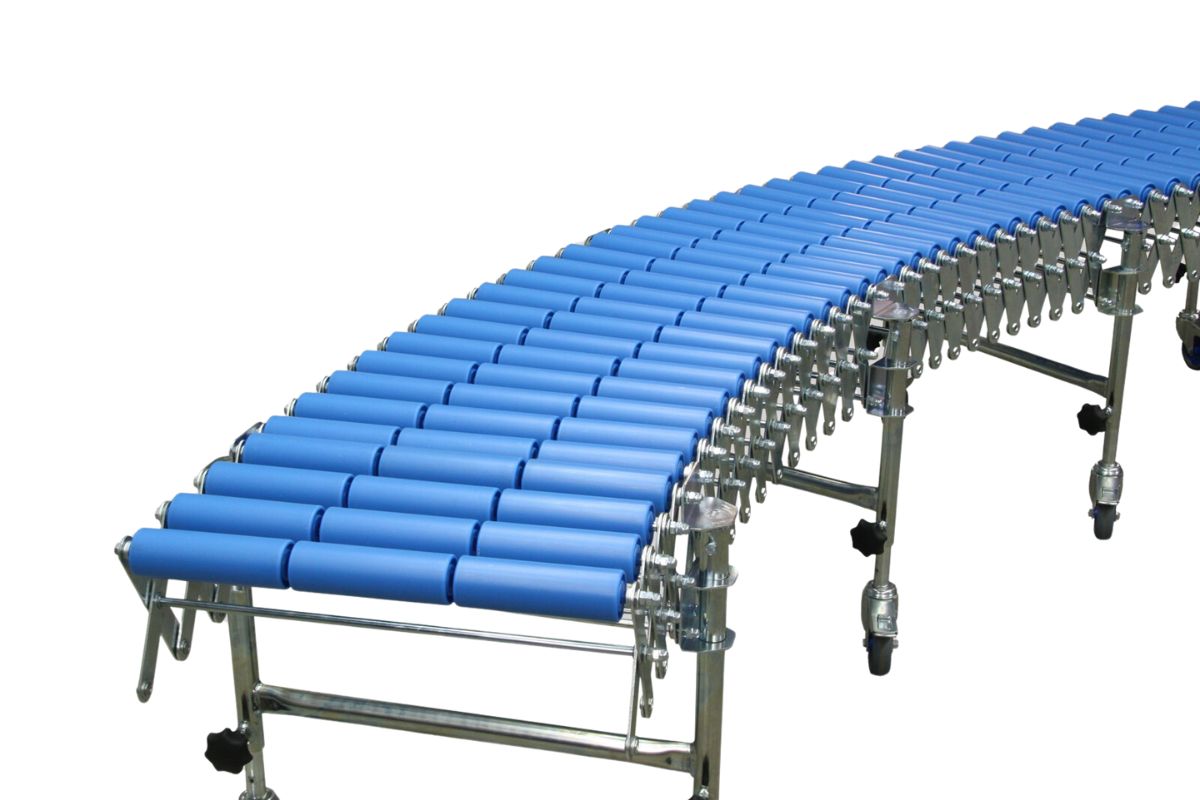
Gravity Roller Conveyor Manufacturer in Panipat
Our gravity roller conveyor systems provide an economical solution for transporting products without external power. These conveyors are widely used in assembly lines, distribution centers, warehouses and production facilities where smooth product movement is essential. Manufactured with precision rollers and heavy-duty frames, they offer excellent durability, low maintenance and high load carrying capacity. We customize roller spacing, frame dimensions and conveyor length according to application requirements, ensuring efficient product handling, faster workflow and improved productivity for industries across Panipat.
Powered Roller Conveyor Manufacturer in Panipat
A Powered Roller Conveyor Manufacturer in Panipat offers motorized conveying systems for businesses that require regular and controlled movement of products. Powered rollers are suitable when loads need to travel automatically over a predetermined route or when manual pushing is not practical.
These conveyor systems can be used in manufacturing units, warehouses, packaging plants, distribution centers, and industrial handling lines. Depending on the application, they can assist with product transportation, accumulation, transfer, and movement between different workstations.
The conveyor is selected according to factors such as load capacity, product dimensions, desired speed, roller specifications, drive arrangement, and operating environment. For more integrated material handling operations, powered roller conveyors can work alongside sensors, transfer equipment, and other automation components.
Motorized Conveyor Rollers in Panipat
Motorized conveyor rollers are designed for intelligent and efficient material movement with consistent speed and excellent load handling capability. These rollers simplify automation, reduce energy consumption and improve production efficiency. Available in different sizes and specifications, they are suitable for warehouses, e-commerce facilities, food processing plants and industrial manufacturing units where reliable conveying performance is essential.
Roller Chain Conveyor Manufacturer in Panipat
Roller chain conveyors are ideal for transporting heavy materials, pallets, drums and industrial products safely and efficiently. Built with strong chains and robust steel construction, these conveyors perform reliably in demanding industrial environments. They require minimal maintenance while delivering consistent performance, making them suitable for engineering, automobile, fabrication and heavy manufacturing industries.
Where Roller Conveyors Are Used
Roller conveyor systems are useful across industries where packaged or unitized materials need to be moved repeatedly. They can be found in engineering and manufacturing plants, textile and packaging facilities, automobile-related industries, warehouses, logistics centers, and dispatch operations.
A conveyor can be used to connect production areas with inspection, packing, storage, or loading points. The layout may include straight sections or customized arrangements depending on the movement path and available installation area.
Benefits of a Well-Planned Roller Conveyor
The main purpose of a roller conveyor is to make internal material movement more organized and less dependent on manual transportation. A suitable system can help maintain a consistent flow between different operational areas and make better use of available workspace.
However, conveyor selection should be based on the actual application rather than simply choosing a standard model. Product weight, dimensions, base condition, conveying frequency, speed, and environmental conditions all influence the appropriate design.
For industrial and commercial facilities in Panipat, a correctly configured roller conveyor can provide a practical solution for everyday material handling. Whether you need gravity movement for simple transfers or powered transportation for a more continuous workflow, the system should be designed around your specific operational requirements.
Specifications
| Material | MS / SS / Aluminium |
| Roller Diameter | As Required |
| Length | Customized |
| Load Capacity | As Per Requirement |
| Application | Material Handling Industries |
What industries use roller conveyors?
Roller conveyors are widely used in warehouses, logistics, automotive, packaging, food processing and manufacturing industries.
Do you provide customized roller conveyors?
Yes, we manufacture customized roller conveyor systems based on your load capacity, dimensions and industrial requirements.
What is the advantage of powered roller conveyors?
Powered roller conveyors improve productivity, reduce manual handling and ensure smooth automated material transportation.